Built for Innovation. Engineered for Scale.
Explore our state-of-the-art manufacturing facilities, advanced R&D laboratories, and world-class infrastructure consistent quality, precision, and reliable agrochemical solutions.
Fully Integrated Production
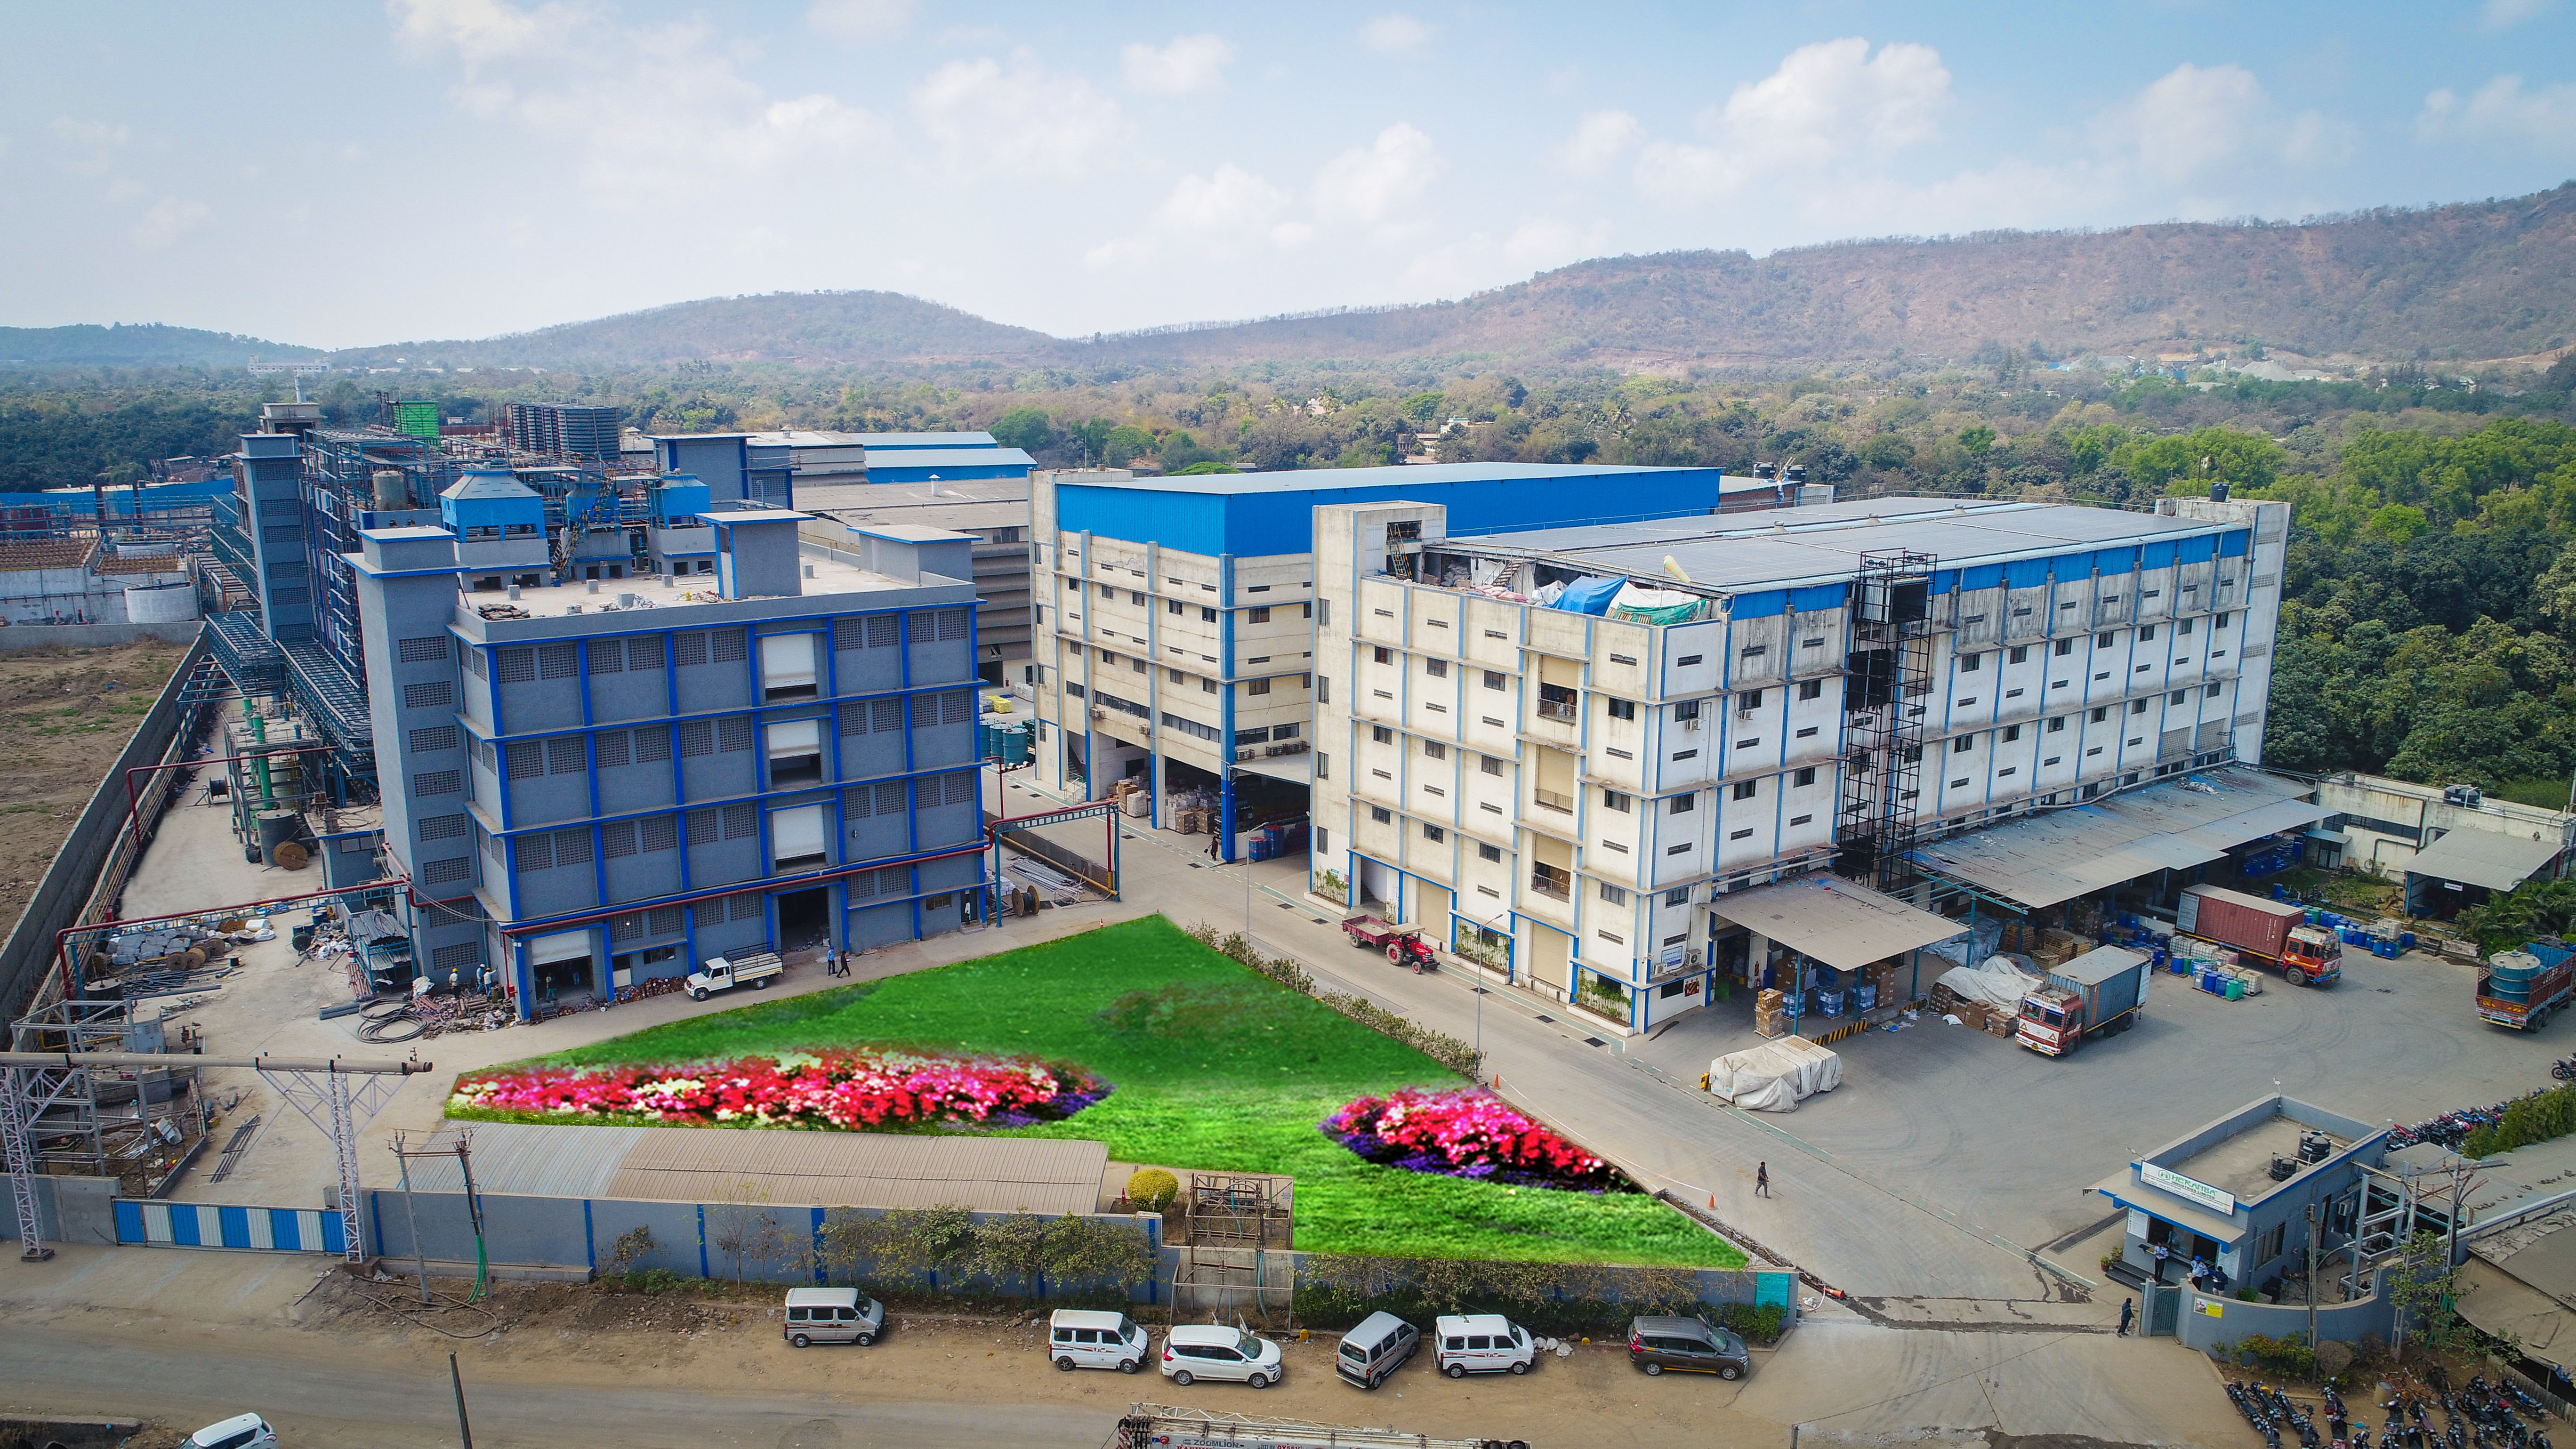
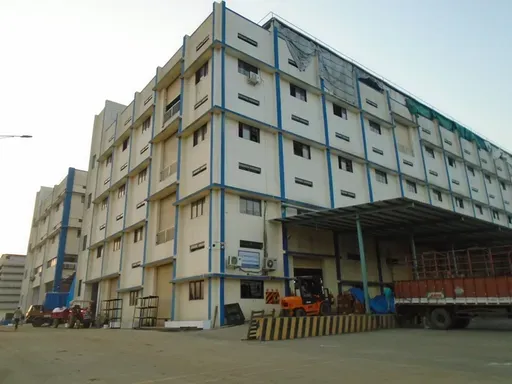
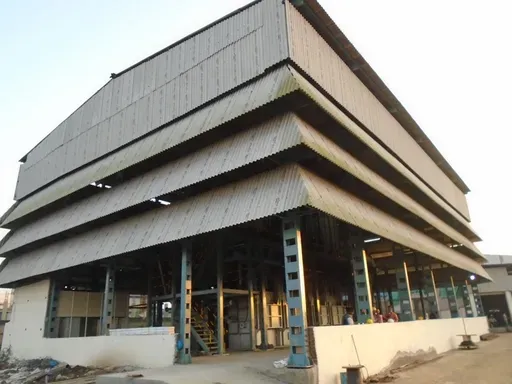
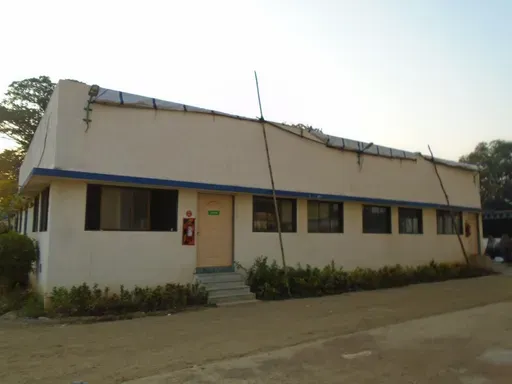
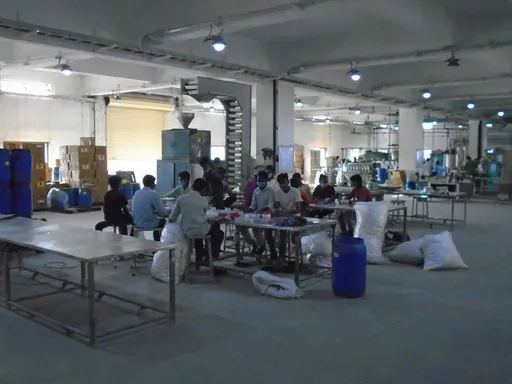
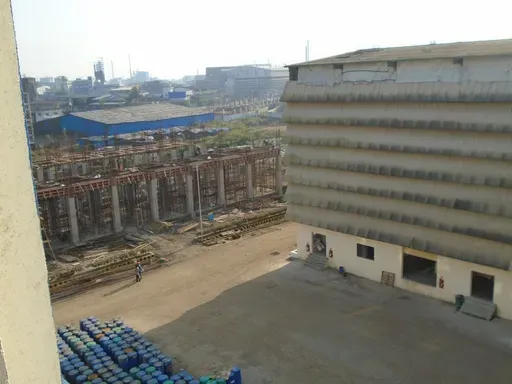
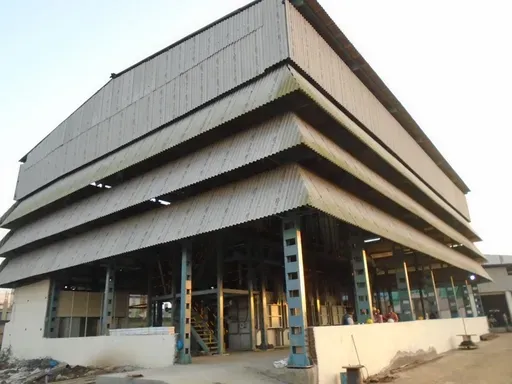
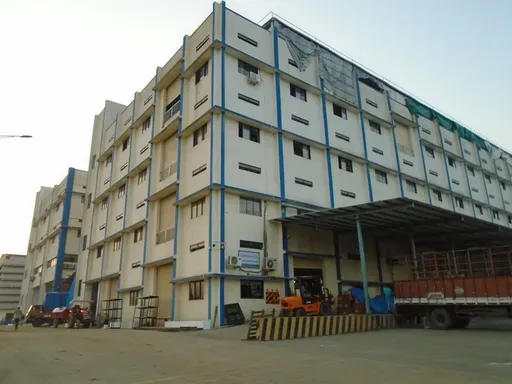
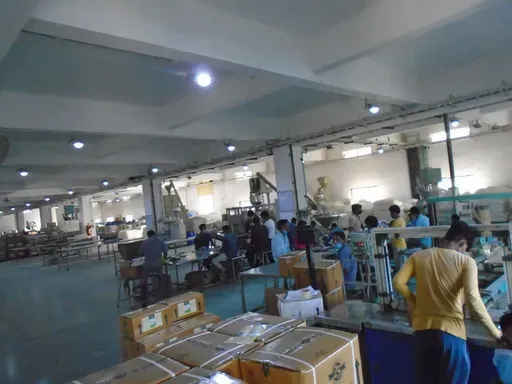
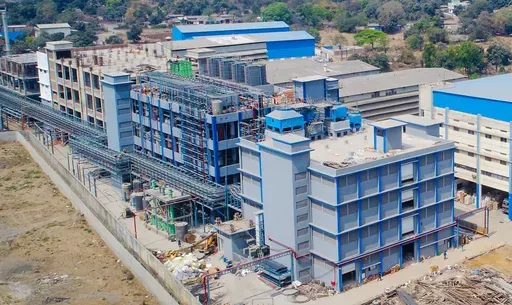
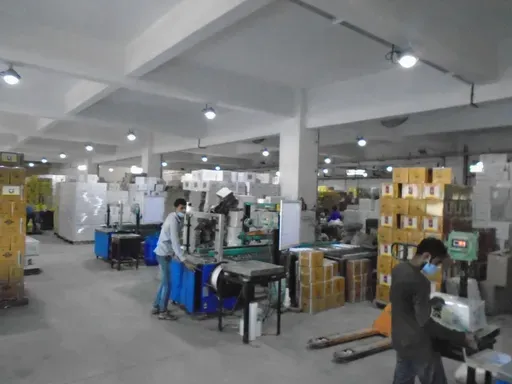
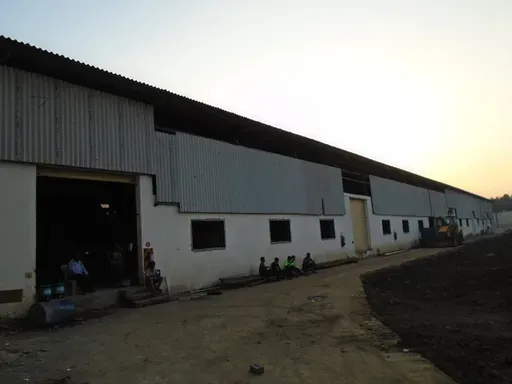
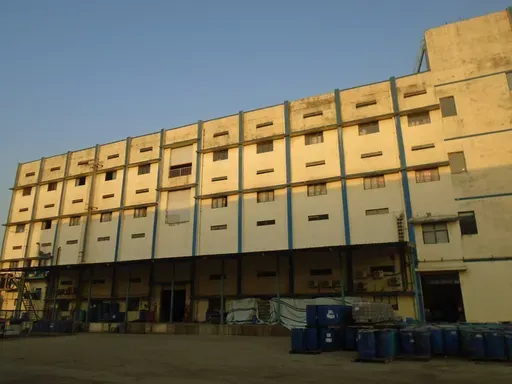
Backed by world-class infrastructure, Heranba Industries Limited operates state-of-the-art manufacturing facilities in the industrial hubs of Vapi and Sarigam (Gujarat), with an upcoming greenfield site at Saykha.
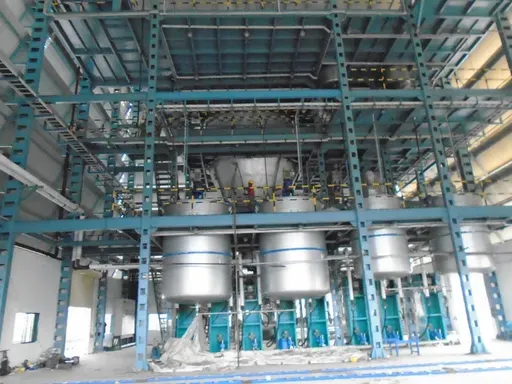
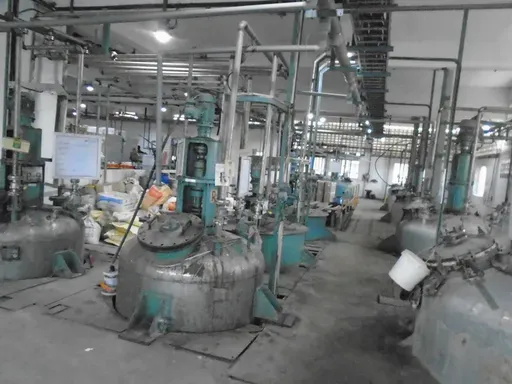
These modern plants are designed to international engineering standards, equipped with DCS automation, and optimized for safe, large-scale chemical processing. Our integrated operations ensure stable raw material supply chains, consistent quality output, and operational flexibility across our entire product portfolio.
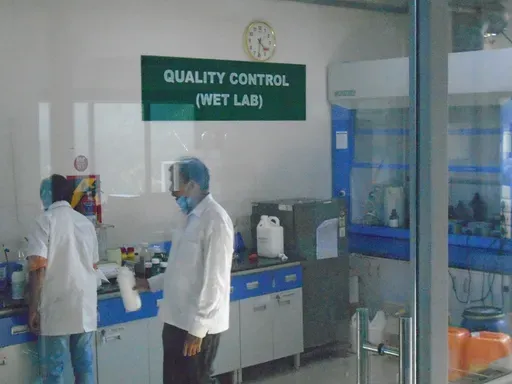
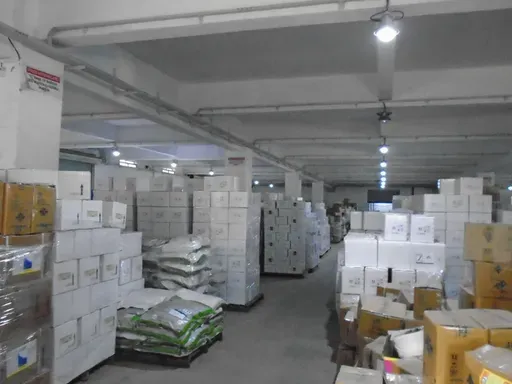
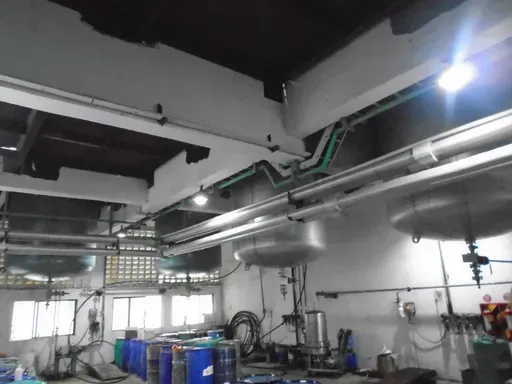
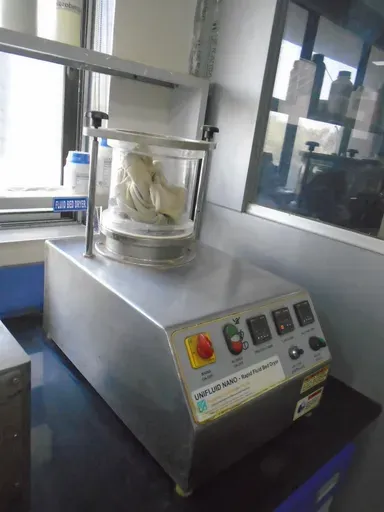
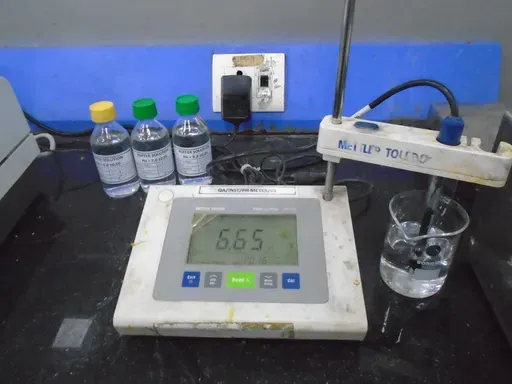
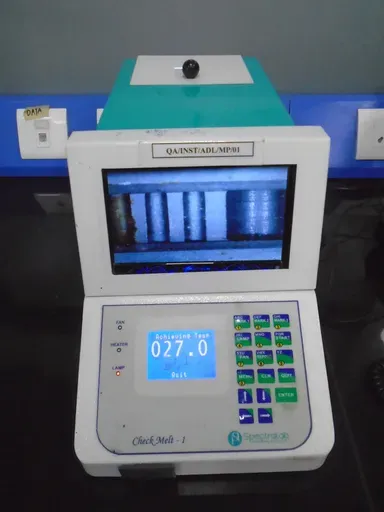
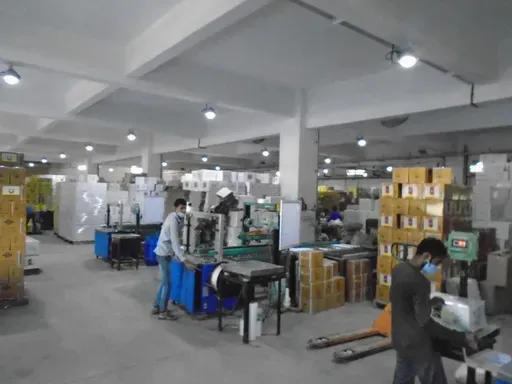
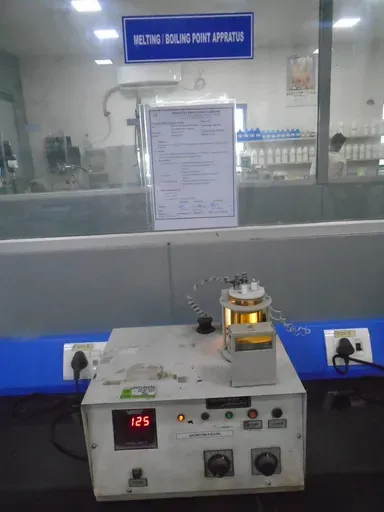
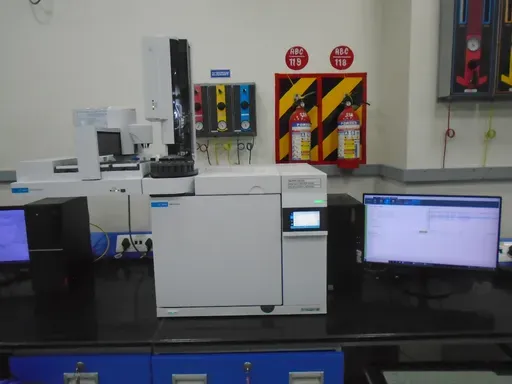
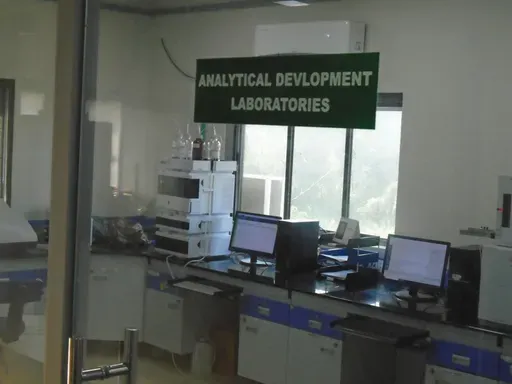
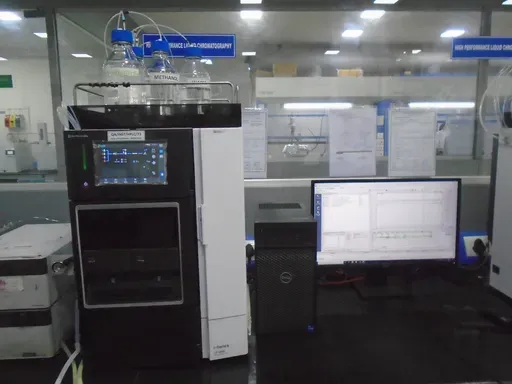
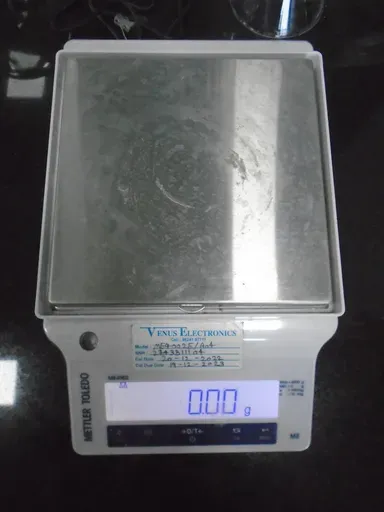
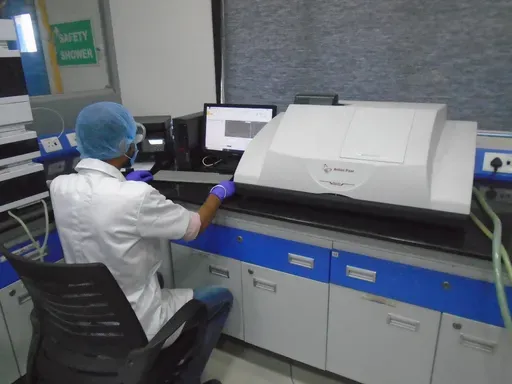
A Glimpse Inside
Explore our state-of-the-art infrastructure ensuring safety, quality, and scale.










































































Site Capacity Comparison
A detailed breakdown of reactor and waste-treatment capacities across our main industrial sites.
| Parameter | Vapi Unit | Sarigam Unit | Saykha Unit (Greenfield) |
|---|---|---|---|
| Site Area | 25,000 sq m | 22,000 sq m | 41,000 sq m |
| ETP Capacity (Effluent Treatment) | 360 KLD | 450 KLD | 320 KLD |
| MEE Capacity (Multi-Effect Evaporator) | 480 KLD | 450 KLD | 250 KLD |
| Boilers Setup | 18 TPH Gas Fired (+ Common Steam) | 20 TPH Coal/Briquette | 16 TPH Coal/Briquette |
| Glass-Lined (GL) Reactors | 82 | 49 | 22 |
| SS-316 Reactors | 65 | 59 | 42 |
| ANFD (Agitated Nutsche Filter Dryer) | 09 | 08 | 06 |
| Centrifuges / CNF | 08 | 04 | 03 |
Reaction Capabilities
Our chemical infrastructure is engineered to execute complex, multi-step organic syntheses safely.
DSIR-Recognized R&D Center
Fostering innovation, process intensification, green chemistry, and custom formulations.
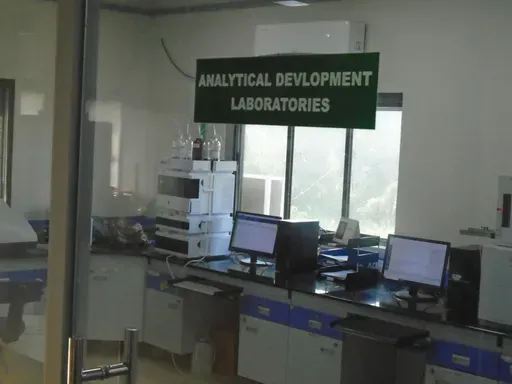
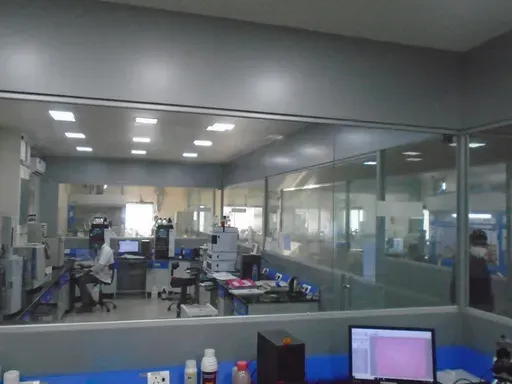
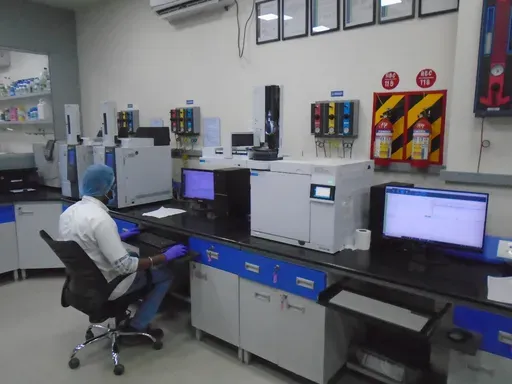
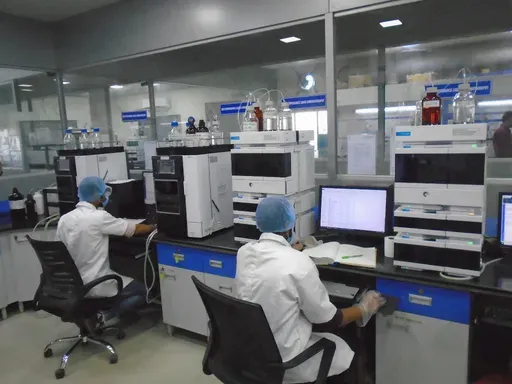
R&D Synthesis & Analytical Labs
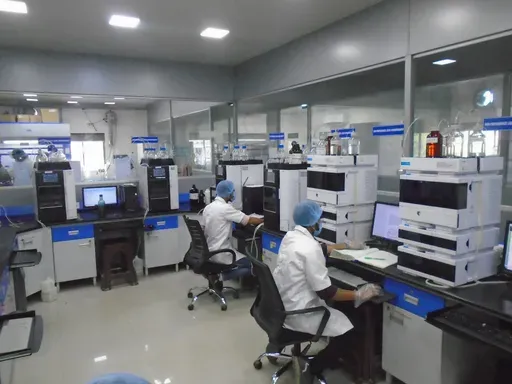
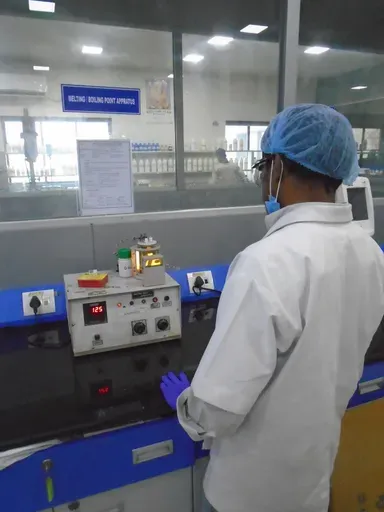
Advanced facilities supporting process development, organic synthesis, and comprehensive analytical evaluation.
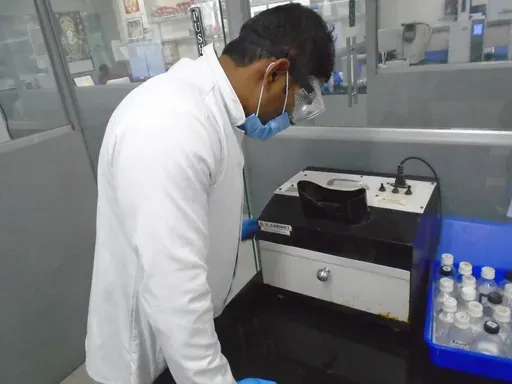
Located across all manufacturing sites with dedicated laboratories for synthesis, process development, and technical support.
State-of-the-art equipment for organic chemical synthesis, including a combined strength of 20+ fume hoods.
High-pressure autoclaves (SS, Glass-Lined & Monel) for critical reactions.
Multidisciplinary R&D team comprising PhDs, MScs, BScs, BTechs, and MTechs.
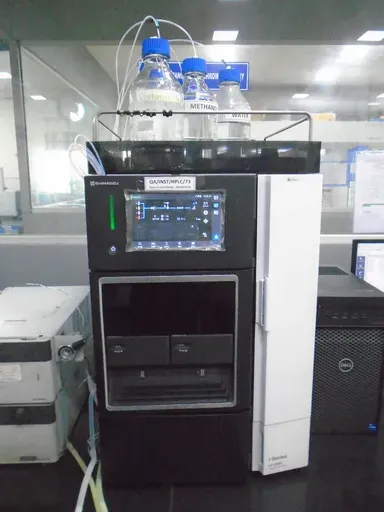
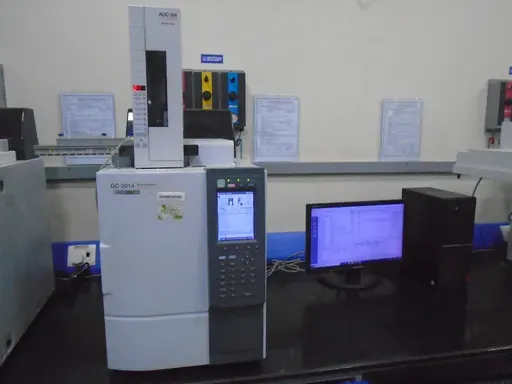
Analytical Equipment
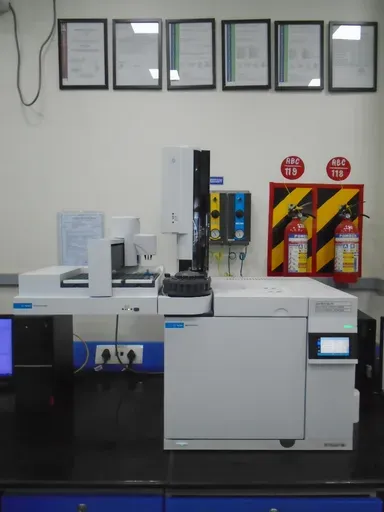
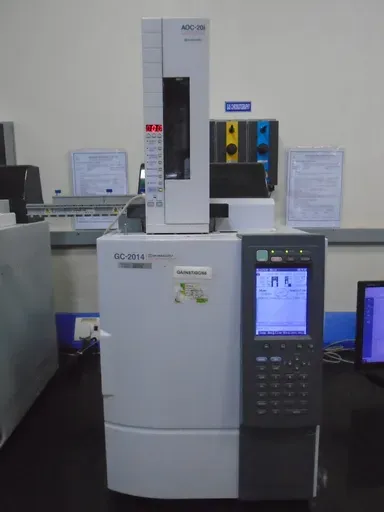
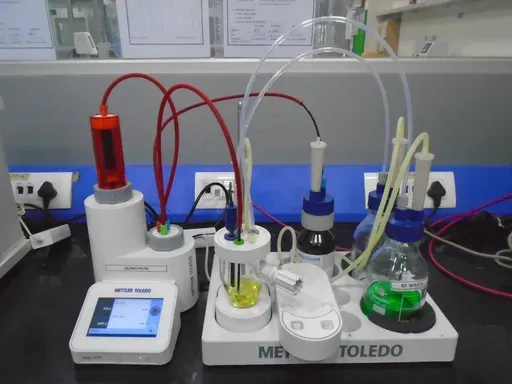
Gas Chromatography (GC), High-Performance Liquid Chromatography (HPLC), Karl Fischer Moisture Analysis, UV–Visible Spectrophotometers, Moisture & Particle Size Analyzers.
Analytical Capabilities
Method Development & Validation, Product Characterization, Process Monitoring, and Stability & Quality Assessment.
Formulation Development Lab
Development of liquid and solid formulations for internal requirements and customer-specific solutions.
Equipment Available
Bead Mill, Air Jet Mill, Extruders, Fluidized Bed Dryer, Spray Dryer, and High-Speed Shearing Agitators.
Key Capabilities
Formulation Optimization, Particle Engineering, Product Performance Enhancement, and Scale-Up Support.
Flow Chemistry Lab
Dedicated facility for novel reaction development and continuous processing technologies.
Equipment Available
Glass CSTR Assemblies, Hastelloy C-276 ARDC Systems, Hastelloy C-276 Pinch Tube Reactors, High-Precision Dosing Pumps, and Static Mixers.
Key Capabilities
Continuous Flow Processing, Process Intensification, Safer Reaction Development, and Technology Transfer Support.
State-of-the-Art Pilot & Scale-Up Facility
Fully functional scale-up Pilot Plants to transition research projects from bench-scale to commercial volumes.
Reactor Systems
Glass-Lined Reactors (250–3000 L) and SS-316 Reactors (250–3000 L) with Anchor & PBT Agitation Configurations.
High-Pressure Systems
High-Pressure SS-316 Autoclaves (up to 140 bar) and Fractionation Column (5 m Packed Height).
Auxiliary Equipment
ANFD SS-316 (150–1500 L), ANFD MS Halar Coated (200 L), Tray Dryer & RVD, MSRL Centrifuge (18"), Scrubbers, High Vacuum Pumps, and Ejectors.
Utility Infrastructure
Cooling Water (32°C), Chilling Water (7°C), Chilled Brine (-20°C), Steam Supply (4 bar), Hot Water (80°C), Hot Oil System (250°C), Air & Nitrogen Distribution Network.
R&D & Process Synthesis Approach
From Laboratory Development to Commercial Manufacturing: Integrated Research, Scale-Up & Commercialization Ecosystem.
Phase 1: Laboratory Development
- Development: Route of Synthesis (ROS) Evaluation, Process Optimization & Yield Enhancement.
- Safety: Safety Assessment (DSC, Dust Explosion, Reaction Calorimetry) and Hazard Identification through Negative Experimentation.
- Validation: Formulation Development & Performance Validation, Solvent Recovery & Waste Minimization, and Scale-Up of Optimized Route for Pilot Validation.
Phase 2: Scale-Up & Commercialization
- Validation: Process Validation at 25–100 kg Scale and Critical Process Parameters (CPPs) Established.
- Engineering: Engineering Evaluation of Mixing, Filtration, Drying & Utilities, and Basic Engineering Package & Technology Transfer Documentation.
- Advanced Tech: Assessment of Advanced Technologies including Flow Chemistry, Liquid Extraction, and Continuous Processing. Foundation Established for Commercial Manufacturing.